Engineered cold-headed fasteners and self-tapping designs optimized for chassis grounding, optical mounting, waterproof seal integrity, and rapid automated robotic feeding.

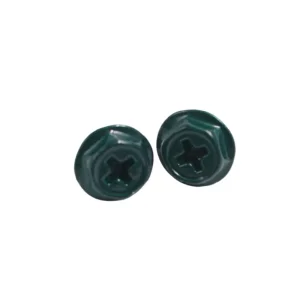
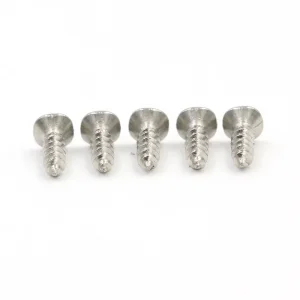
In high-density electronics manufacturing, mechanical fasteners are not mere hardware; they are critical thermal paths, electrical grounding bridges, and environmental barriers that dictate device longevity.
The concentration of cold-heading, multi-station tooling, precision wire drawing, and plating ecosystems within the Pearl River Delta (Dongguan cluster) provides unmatched economies of scale, compressing new tooling lead times to under 10 business days.
Global electronics OEMs demand defect rates below 5 PPM (Parts Per Million). Tier-1 Chinese manufacturers utilize glass-plate automated optical inspection (AOI) with multi-angle telecentric lenses, screening 1,200 parts/min across 16 critical geometric dimensions.
Despite diversification strategies (China+1), Chinese electronics fastener factories maintain unmatched supremacy in advanced metallurgy, specialized micro-thread profiles (PT/Delta PT equivalent), and micro-surface finishing capable of exceeding 1,000 hrs salt spray.
Design Insight for Hardware Engineers: Micro-fastener failure during automated high-speed torque installation is overwhelmingly attributable to non-concentric drive recesses or improper case depth. Precision cold-heading dies engineered to JIS B 1059 and ISO 10664 standards ensure driver bit cam-out prevention and consistent clamp loads across multi-spindle automatic screw feeding robots.
A granular breakdown of mechanical fastening architectures deployed across consumer telecommunications, automotive electronics (ADAS/BMS), and industrial automation enclosures.
| Fastener Classification | Predominant Materials | Drive & Head Configurations | Critical Engineering Attributes | Target Electronics Subsystem |
|---|---|---|---|---|
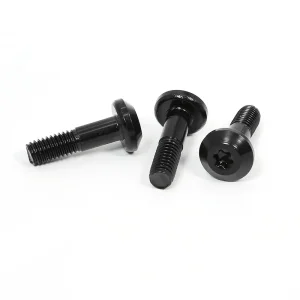
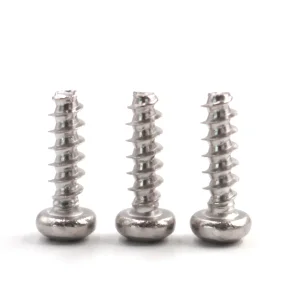
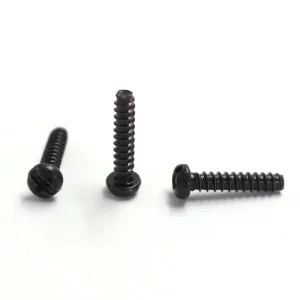
| Micro Thread-Forming (PT/Delta PT) | Case-Hardened Carbon Steel (1022A), SUS410, SUS304 | Torx (6-Lobe), Phillips Pan, Low-Profile Wafer | 30° flank angle reduces radial hoop stress in engineered thermoplastics (PC/ABS, PBT, LCP). Prevents boss rupture. | Smartphone frames, drone gimbal housings, smart meter casings, optical sensor brackets. |
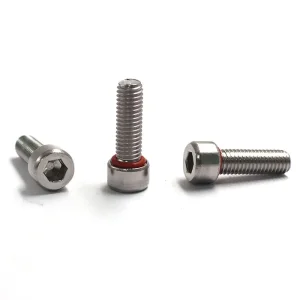
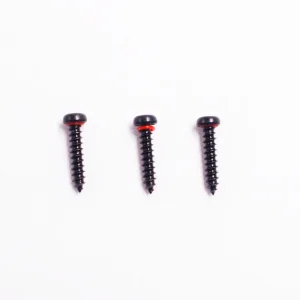
| Hermetic IP67/IP68 Sealing Screws | SUS304, SUS316, Grade 8.8 Alloy Steel | Under-head engineered groove with NBR, FKM (Viton), or Silicone O-ring | Provides 360° metal-to-metal contact while uniformly compressing the elastomer seal against internal pressures up to 10 MPa. | Outdoor telecommunications (5G RRU), EV battery pack modules, LiDAR housings, underwater acoustic sensors. |
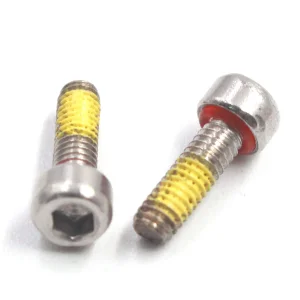
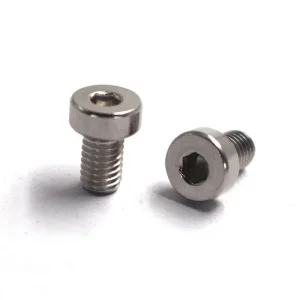
| Pre-Applied Prevailing Torque (Nylon Patch) | SUS302, SUS304, High Tensile Alloy Steel | Socket Head Cap, Flat Countersunk, Shoulder Stepped | 180° or 360° Polyamide 11 patch creates resilient interference fit. Reusable up to 5 installations without losing retention torque. | Vibrational assemblies, industrial robotic wrist joints, micro servo motors, PCB dynamic retainers. |
| Captive Fasteners & Sems Combinations | Carbon Steel (Zinc/Nickel plated), Austenitic Stainless Steel | Cross-recessed pan with integral helical spring & flat washer (SEMS) | Eliminates loose hardware risks during maintenance. Retains washer assembly mechanically prior to thread rolling. | Data center server blades, telecom power distribution units (PDU), industrial PLC control cabinets. |
| Precision Ball & Spring Plungers | SUS303 Housing, SUS304 Ball, Piano Wire Spring | Slotted, Hex Socket, Press-Fit Flanged Housing | Calibrated repeatable detent resistance (N ±10%). Micro-stroke positioning for tactile feedback and indexing mechanisms. | Camera lens bayonet mounts, modular switchgear, medical diagnostic sliding stages, robotic end-effectors. |
Traditional flat washers deform under torque, extruding elastomeric materials outward. Our custom self-sealing screws feature cold-headed under-head annular recesses that mechanically encapsulate the O-ring, ensuring uniform seal volume displacement and zero fluid bypass under cycling temperatures from -40°C to +150°C.
As fast-moving electronic designs transition to M1.2 and smaller fasteners, traditional Phillips drives present severe cam-out risks. By utilizing cold-headed Torx (ISO 10664) and Torx Plus 6-lobe configurations, driving angle engagement drops to 15°, reducing driver down-force requirements by 80% and mitigating bit wear.
High-tensile carbon steel electroplated fasteners (Class 8.8, 10.9, 12.9) are intrinsically susceptible to delayed brittle failure triggered by atomic hydrogen absorption during acid pickling and electroplating. YH Fastener mandates immediate post-plating thermal de-embrittlement baking at 200°C–220°C for 4 to 12 hours.
Ensuring galvanic compatibility, non-magnetic performance, and zero chemical outgassing inside sensitive semiconductor and optical enclosures.
Provides an amorphous, uniform nickel-phosphorus alloy barrier (6–9% P) over complex threads, eliminating thread thickness build-up while achieving 400+ hrs neutral salt spray resistance and exceptional wear characteristics.
Trivalent chromium passivation (RoHS compliant) engineered specifically for optical enclosures, laser housings, and camera modules requiring non-reflective matte or semi-gloss finishes without micro-flaking risks.
Using premium low-permeability SUS304 and SUS316 austenitic stainless wires (magnetic permeability µ < 1.02), cold-headed with custom anti-work hardening annealing to eliminate magnetic interference in RF and Hall-sensor assemblies.
Multi-stage automated ultrasonic degreasing using deionized water cascades, followed by vacuum drying and antistatic Class 1,000 / Class 10,000 cleanroom packaging to satisfy strict particle-count limits for wafer and hard-drive manufacturing.
Regulatory Compliance Commitment: All electronics fastening parts manufactured at Yu-Huang Electronics fully comply with EU RoHS Directive 2011/65/EU and its amendment (EU) 2015/863, REACH (EC No 1907/2006) for Substances of Very High Concern (SVHC), Dodd-Frank Act Section 1502 Conflict Minerals reporting (CMRT standard), and California Proposition 65.
How tailor-made mechanical fasteners solve high-stress thermal, vibrational, and environmental challenges across leading technological sectors.
Challenge: Severe mechanical shock, wide temperature oscillations (-40°C to +125°C), and copper-to-aluminum busbar galvanic corrosion.
Solution: Custom M4 flanged sems screws with zinc-nickel alloy plating (15% Ni) paired with pre-assembled Belleville spring washers that maintain continuous clamp preload despite thermal expansion and contraction cycles.
Challenge: Wind-load vibrational loosening and long-term coastal corrosion demanding IP68 ingress protection on cast aluminum enclosures.
Solution: SUS316 precision self-sealing machine screws featuring cold-headed underhead O-ring grooves and micro-encapsulated threadlocker, achieving 1,500 hours ASTM B117 salt spray endurance without clamp degradation.
Challenge: Micro-backlash in multi-axis robotic articulation joints and rapid detent positioning wear.
Solution: High-precision stainless steel ball spring plungers with heat-treated SUS440C hardened steel balls and calibrated piano wire springs, providing consistent 4.5N indexing force over 500,000 continuous cycling engagements.
Anticipating the technological demands of ultra-miniaturized smart wearables, humanoid robotics, quantum computing cryogenics, and circular closed-loop manufacturing.
Development of commercial cold-heading tooling systems for M0.6 and M0.8 titanium (Ti-6Al-4V) and exotic nickel superalloys. Transitioning wearable medical electronics and AR/VR head-mounted displays toward ultra-lightweight, bio-compatible micro-fastening systems with zero skin-irritation risk.
Deployment of generative edge-AI machine vision algorithms integrated with multi-spectral sorting carousels. Real-time sub-surface micro-crack detection, 360-degree internal thread contour verification, and automatic tool-wear compensation in cold-heading multi-die stations.
Fastening architectures engineered specifically for superconducting quantum computing enclosures operating below 4 Kelvin. Implementation of 100% green-hydrogen annealed wire drawing, circular scrap reclamation, and biodegradable pre-applied prevailing torque chemical compounds.
In-depth responses covering tolerances, tooling parameters, environmental testing, and engineering validation.
Our standard production achieves ISO 4759-1 Class A tolerances. For precision micro screws (M1.0 to M3.0), we regularly hold shank and major diameter tolerances within ±0.03 mm, length tolerances within ±0.10 mm, and head concentricity within 0.05 mm TIR (Total Indicator Reading). High-precision Swiss-type CNC post-machining is available for ultra-critical applications requiring ±0.005 mm tolerances.
We configure thread geometries specifically for thermoplastic resins. Our PT and Delta PT equivalent thread-forming screws utilize an acute 30° flank angle compared to standard 60° machine threads. This cuts radial stress by approximately 50%, maximizes plastic displacement into the thread valley, elevates strip-to-drive torque ratios to 3.5:1 or higher, and mitigates plastic boss blowout during high-RPM automatic screwdriving.
Our plants operate under ISO 9001:2015, ISO 14001:2015, and IATF 16949:2016 quality management systems. Every shipment is backed by raw material mill test certificates (chemical composition and mechanical properties), optical sorting dimensional inspection reports, plating thickness x-ray verification, salt spray chamber test logs, and PPAP Level 3 documentation upon request.
A nylon patch (Polyamide 11) is a mechanical prevailing torque solution; it provides reusable friction retention without chemical curing and functions instantly across a wide temperature range (-50°C to +125°C). Micro-encapsulated adhesive (such as 3M or Precote) is a reactive chemical threadlocker that crushes during installation, fully curing in 24 hours to create an airtight, high-breakaway torque bond that is non-reusable without re-application.
We support prototype development through dedicated sample-shop cold headers and Swiss CNC machines, supplying 100 to 5,000 pilot qualification parts in as little as 7 to 10 days with production-intent materials. Once approved, our high-speed multi-station headers seamlessly scale to production capacities exceeding 50 million units per month.
Explore engineered industrial machine bolts, fine-thread stainless tapping screws, anti-loosening shoulder screws, and spring detent plungers for ruggedized assemblies.
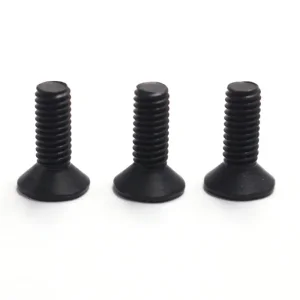

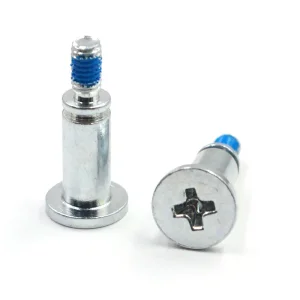

Upload your 2D CAD drawings (DWG/PDF) or 3D STEP models to receive a comprehensive Design for Manufacturability (DFM) review and formal cost quote within 24 hours.
