Engineered for direct installation into plastics, non-ferrous metals, sheet stampings, and structural assemblies without preliminary tapping.
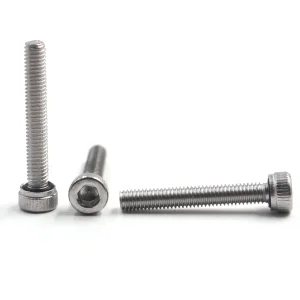
304 Stainless steel with integrated rubber elastomer groove designed for hermetic IP67 enclosure integrity.

Engineered cross-recess pan head with fluid sealing mechanics for high-vibration battery and control enclosures.
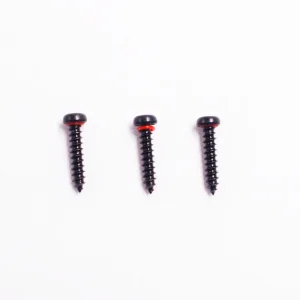
Electrophoretic black finish coupled with heat-resistant O-rings providing instantaneous sealing during thread forming.
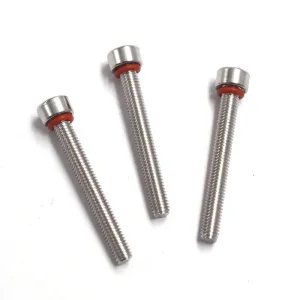
Austenitic alloy design engineered to eliminate moisture pathways in saltwater exposure and marine enclosures.
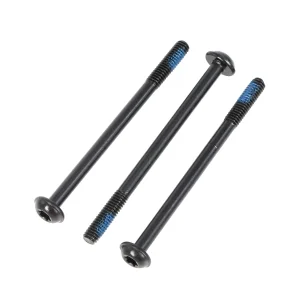
Prevailing-torque 360° or 180° nylon patch deposition preventing vibrational back-out in dynamic drive units.
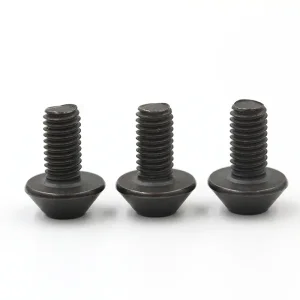
Class 4.8 to 12.9 carbon steel with blue zinc electro-plating for structural industrial equipment assemblies.
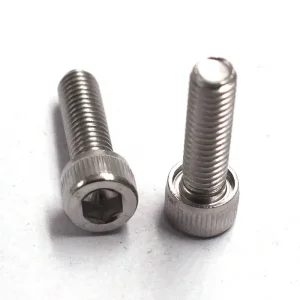
Standard and tight-tolerance custom metric socket head cap screws designed for uniform preload clamping.
Full-process cold heading across unified coarse/fine and metric pitch systems for international cross-compatibility.
Analyzing Cold Heading Kinematics, Substrate Plasticity, and Global Supply Optimization
Unlike conventional cut tapping, modern thread-rolling (forming) creates a zero-clearance internal mating thread via plastic deformation. This process causes grain structure flow along the profile contours, yielding high pull-out resistance, superior fatigue life, and zero chip contamination in cleanroom and electronic setups.
To combat boss bursting in brittle thermoplastics and light casting alloys (e.g., magnesium and cast aluminum), custom trilobular geometries create localized yield relief zones. This substantially drops driving torque while retaining peak break-away and stripping ratios across high-speed robotic screwdriving operations.
Effective self-tapping performance mandates dual-tier metallurgical control: a surface case depth of 450–750 HV for thread generation against tough counter-substrates, backed by a ductile core structure (280–380 HV) to absorb dynamic shear vectors and mechanical vibration without brittle failure.
Eliminating supply bottlenecks through multi-tier internal routing: cold heading, high-speed thread rolling, in-house carburizing, and automated optical validation.
Equipped with 3-die 3-blow, 4-die 4-blow, and 6-die multi-station cold heading configurations in our Dongguan, Shaoguan, and Wuhan plants. High-speed progressive forming minimizes cold-work stress fractures while optimizing continuous metallurgical flow lines.
Automated glass turntable visual sorting systems verify 100% of fastener outputs across critical parameters: head diameter, recess concentricity, pitch angle, thread lead, and washer sealing seating, eliminating line downtime on high-volume automated lines.
Every batch links back directly to raw wire rod mill heats (Baosteel, Walsin Lihwa). Full spectrometer element reporting, salt spray testing data, microhardness profiles, and tensile load sheets accompany every commercial delivery batch under IATF 16949 control.
Mechanical profiles and substrate matching reference for precision design engineers and OEM procurement teams.
| Thread Type Standard | Profile Geometry | Target Substrate Material | Installation Dynamics | Pre-Applied Functional Cores |
|---|---|---|---|---|
| Type AB / B | Wide spaced, gimlet or blunt point (ISO 1478) | Thin Sheet Metal (≤1.2mm), Plywood, Resin Panels | Fast initial pitch pickup; high thread flank engagement | Zinc + Cr3+ passivate, Black Nickel, Dacromet |
| PT® / TP Thread for Plastic | 30° or 45° asymmetric flank angle; trilobular | Thermoplastics (ABS, PA66, PBT, Polycarbonate) | Minimal radial stress; prevents boss cracking; low drive torque | Integrated elastomeric O-rings, Nylon thread patch |
| Type F / Type 23 Cutting | Machine pitch with swarf chip relief flutes | Die Cast Zinc, Aluminum Alloy, Structural Plastics | True cutting action; creates full matching machine threads | High corrosion multi-layer zinc-nickel, dry lubricant film |
| Taptite® Thread Rolling | Tri-roundular cross section with burnishing lobes | Ductile Metals, Carbon Steel Plate, Stamped Brackets | Work-hardens mating internal thread; superior clamp retention | Micro-encapsulated adhesive, sealing under-head gaskets |
Precision fasteners manufactured for automotive powertrain modules, commercial electronics enclosures, and structural hardware assemblies.

Thread cutting fastener engineered for high mechanical retention in electrical and structural equipment.
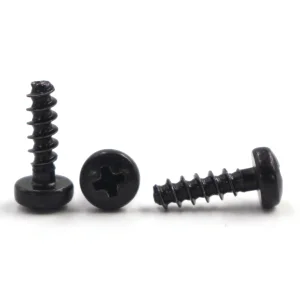
Engineered TP thread geometry in 304/316 and carbon steel preventing radial hoop stress failure in polymeric housings.

Zinc plated flat head countersunk design delivering flush seat engagement across industrial timber and panel assemblies.
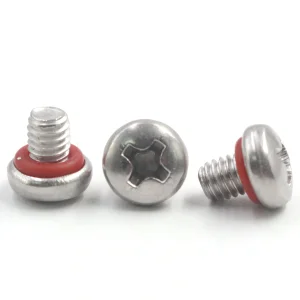
Precision CNC or cold-headed under-head containment track for consistent elastomeric O-ring compression.
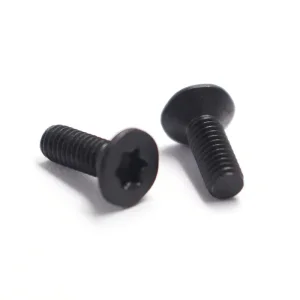
High precision countersunk machine screws manufactured to DIN/ISO standards for smooth industrial finishes.
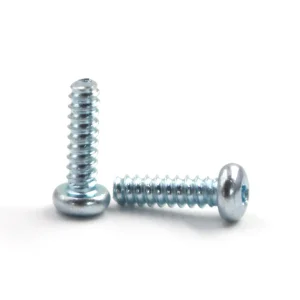
Six-lobe drive configuration preventing cam-out alongside PT profile engineered for new energy vehicle assemblies.

Corrosion-resistant stainless steel self-tapping fasteners for high-speed automated manufacturing lines.

Specialized chemical-resistant plating on ultra-fine thread paths for sensitive consumer electronics and automotive ECUs.
Engineered fasteners addressing specialized technical challenges across modern global manufacturing sectors.
Applied in battery pack tray structural assembly, inverter heat sink attachments, and sensor bracket installations. Self-tapping trilobular fasteners eliminate metal scrapings that cause short circuits, while maintaining high residual clamping tension during continuous road vibration.
Miniature micro-fasteners down to M0.8 and M1.2 sizes engineered for smartphone internal chassis, 5G base station filtering modules, and optical transceivers. Strict electro-less nickel finishes meet 0.002mm thread pitch accuracy requirements without hydrogen embrittlement hazards.
Bi-metal self-drilling and thread-tapping screws combining a carbon steel drill tip with a 316 austenitic stainless body. Delivers high corrosion endurance (>2,000-hour neutral salt spray) for outdoor photovoltaic framing and harsh coastal deployments.
Clear, direct answers to common questions about thread geometry, surface processing, and custom manufacturing.
Send our application engineering team your CAD models, bill of materials, or interface load specs. Receive a comprehensive manufacturing feasibility report and tooling estimate within 24 hours.
Connect with a Fastener Engineer