Engineered for automotive battery enclosures, IP67/IP68 industrial electronics, and structural flush installations requiring zero leakage and persistent anti-loosening torque.


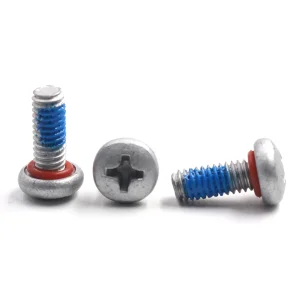
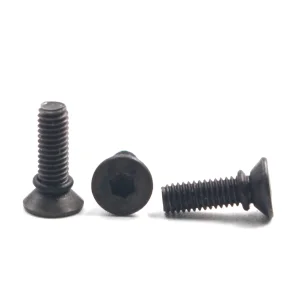
How precision machining, underhead elastomeric groove geometry, and controlled preload achieve zero-clearance fluid and gas isolation without compromising structural load paths.
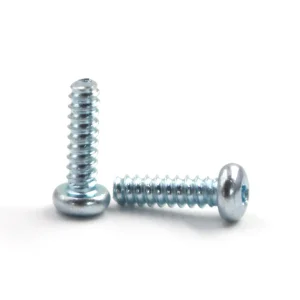
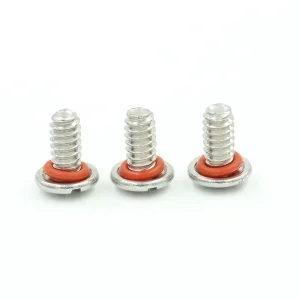
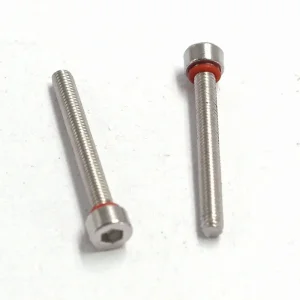
In modern electromechanical, aerospace, and energy storage architectures, space optimization and aerodynamic integrity demand fastening solutions that sit entirely flush with the mating surface. However, standard flat-head fasteners create an open clearance path along the conical contact interface. When exposed to internal hydraulic pressures, chemical washdowns, or external environmental contamination, non-sealing countersunk joints allow rapid ingress or fluid leakage. Countersunk sealing screws (often specified as flat-head self-sealing machine screws) eliminate this failure mode by integrating an elastomeric O-ring or molded vulcanized seal into an engineered groove under the 90°, 100°, or 120° conical head.
Achieving a reliable, hermetic seal on an angled surface is far more complex than on a flat pan or cheese-head fastener. In a flat under-head configuration, compression forces act uniformly normal to the sealing surface. Conversely, on a countersunk head, axial installation torque generates multi-vector force components: normal compressive stress against the chamfer and radial shearing forces that attempt to extrude or dislodge the elastomeric ring up the mating bore. Yu-Huang Electronics (YH Fastener) has resolved this kinematic challenge through precision CNC micro-grooving and cold-heading heading geometries that establish a controlled confinement cavity. This ensures the elastomeric element reaches an optimal 25% to 32% volumetric squeeze without experiencing mechanical pinch, creep, or premature shear during tightening.
Critical Engineering Principle: A countersunk sealing fastener must achieve full metal-to-metal contact along the top bearing perimeter while strictly containing the compressed elastomer within its designated annular under-head recess. This ensures structural torque retention and preload stability while guaranteeing IP68 ingress protection up to 6,000 PSI internal hydrostatic pressure.
Beyond fluid containment, countersunk sealing screws serve an essential role in preserving laminar air and fluid flows in exterior assemblies, preventing snagging in compact modular rack enclosures, and isolating dissimilar metals against galvanic corrosion. Whether utilizing fluorocarbon (Viton™), silicone, Buna-N (NBR), or EPDM sealing rings, the mating interfaces must be machined with tight surface finishes (Ra 0.8 µm or better) to prevent micro-leakage across microscopic machining grooves.
Precision cold-headed or micro-turned under-head grooves calculated precisely for elastomer thermal expansion without excessive volume swell or seal blowout.
Material compatibility options spanning high-temperature fluorosilicone (-60°C to +200°C), automotive fuel-resistant Viton, and FDA-compliant medical grade elastomers.
Available in high-torque Torx (six-lobe), Torx Plus, tamper-resistant pin, and traditional slotted/Phillips cross recess drives to eliminate driver cam-out in high-speed lines.
Austenitic A2/A4 stainless steels (SS304/SS316), heat-treated high-tensile alloy steels (Grade 8.8, 10.9), and lightweight aerospace titanium grades with anti-galling coatings.
Integrating multi-station cold-forming, in-house tooling creation, automated optical sorting, and direct elastomeric bonding under a single roof across 20,000 m² of modern industrial infrastructure.
Global original equipment manufacturers and Tier-1 automotive integrators face severe supply chain bottlenecks when sourcing specialized sealing hardware from Western suppliers, who often outsource secondary operations like O-ring grooving, heat treating, or chemical plating to disparate third parties. Yu-Huang Electronics Dongguan Co., Ltd. (YH Fastener) revolutionizes this paradigm by consolidating the entire lifecycle of countersunk sealing fastener production across its three major manufacturing bases in Dongguan, Shaoguan, and Wuhan, China.
Operating over 20,000 square meters of specialized workshop space with more than 30 years of fastener manufacturing heritage, YH Fastener combines rapid prototyping speed with massive production volume. Utilizing multi-station cold heading machines imported from Taiwan and Japan, our facilities form miniature M1.6 micro-screws up to heavy-duty M12 industrial fasteners at speeds exceeding 120 to 300 pieces per minute. Cold heading preserves continuous metallurgical grain flow along the screw shank, head transition, and threads—yielding tensile and shear strengths up to 25% superior to fully machined alternatives while dramatically minimizing raw material scrap.
Furthermore, the Pearl River Delta industrial ecosystem affords unparalleled supply chain synchronization. Raw material wire rod (sourced from premier domestic and international steel mills with complete heat-lot traceability) is drawn, spheroidized, and cold-headed within an optimized logistics radius. Secondary surface treatments—such as zinc-nickel alloy plating with 1,000+ hour neutral salt spray resistance (ASTM B117), electroless nickel, black trivalent passivations, and mechanical zinc deposits—are strictly controlled in compliant, environmentally certified finishing plants. By managing tooling fabrication, secondary CNC grooving, automated optical sorting, and pre-applied adhesive or elastomeric ring assembly under one management system, YH Fastener consistently shrinks standard lead times by 30% to 50% compared to regional competitors.
Multi-stage progressive dies shape complex countersunk head cavities and O-ring detention grooves simultaneously, guaranteeing structural grain continuity and eliminating internal stress concentrations.
High-speed glass-disc optical sorting tables verify thread pitch, shank straightness, drive recess depth, and O-ring seating integrity, filtering dimensional defects down to <50 PPM.
Every batch is backed by EN 10204 3.1 chemical analysis, tensile testing, core hardness logs, and coating thickness records verified by in-house X-ray fluorescence spectroscopy.
Bridging the gap between Chinese factory direct manufacturing and stringent international regulatory requirements across North America, Europe, and the Asia-Pacific.
Supplying multinational Tier-1 corporations and OEMs in mission-critical industries requires total adherence to documented quality frameworks. YH Fastener operates under rigorous ISO 9001:2015, ISO 14001:2015, and IATF 16949:2016 quality management certifications. For automotive, defense, and life science programs, our application engineering team executes complete Production Part Approval Process (PPAP Level 1 through Level 5) packages, incorporating Process Flow Diagrams, Process Failure Mode and Effects Analysis (PFMEA), Control Plans, and Measurement Systems Analysis (MSA) studies.
In addition to quality process management, all material compositions and chemical surface treatments comply fully with European and global environmental directives, including EU RoHS (Restriction of Hazardous Substances 2011/65/EU and its amendment 2015/863), REACH (Regulation EC 1907/2006 for Substances of Very High Concern - SVHC), and California Proposition 65. Detailed full material declarations (FMD) are uploaded directly into the International Material Data System (IMDS), guaranteeing effortless verification for global automotive procurement platforms.
| Performance Dimension | Standard / Verification Method | YH Fastener Capability Benchmark | Industry Compliance Standard |
|---|---|---|---|
| Hermetic Seal Ingress | ISO 20653 / IEC 60529 | IP67, IP68, IP69K (High-Pressure Thermal Washdown) | Full In-House Immersion Tested |
| Automotive APQP / PPAP | AIAG Manual 4th Edition | PPAP Level 3 Standard (PSW, FMEA, Gage R&R, CPK > 1.67) | IATF 16949 Certified |
| Corrosion Resistance | ASTM B117 / ISO 9227 | Up to 1,500 hours neutral salt spray to red rust (Zn-Ni) | RoHS / REACH Compliant |
| Preload Torque Retention | DIN 65151 (Junker Test) | Custom pre-applied micro-encapsulated polyamide patches | Prevailing Torque Spec |
| Material Traceability | EN 10204 Type 3.1 | Full heat-treat batch records, spectral composition analysis | 100% Heat-Lot Control |
| Dimensional Quality | ISO 2859-1 / Zero-Defect | Multi-camera telecentric optical sorting (<50 PPM) | Automated Screening |
To eliminate timezone latency and communication friction, YH Fastener maintains dedicated bilingual engineering pods available 24/7. When engineering teams in Detroit, Munich, Tokyo, or London submit complex 2D technical drawings (AutoCAD, PDF) or 3D CAD step files (SolidWorks, CATIA, STEP, IGES), our senior mechanical designers deliver a comprehensive Design for Manufacturability (DFM) review within 24 hours. This includes recommendations on counterbore depth tolerances, lead chamfer radii, mating countersink angle matching (e.g., 90° vs 100° aerospace vs 82° ANSI), and elastomer compression calculations to avert costly re-tooling iterations.
From electric vehicle lithium-ion battery enclosures to deep-sea oceanic telemetry, countersunk sealing screws ensure structural security without allowing a single droplet of moisture or gas penetration.
Flush installation on underside chassis trays avoids ground obstacle strikes while maintaining airtight IP67/IP68 containment to prevent battery thermal runaway triggered by road spray or humidity infiltration.
Used in remote radio units (RRU) and outdoor distributed antenna housings, sealing against heavy tropical rain, driving blizzards, and internal nitrogen or dielectric gas purge loss over 20+ years.
Marine navigation consoles, sonars, and underwater camera domes require A4/316L stainless steel countersunk sealing screws capable of withstanding saltwater hydrostatic loads up to 450 bar without crevice corrosion.
Ensures autoclave and caustic enzymatic washdown fluids do not compromise sensitive multi-axis surgical robotics, fluidic pumps, and hermetic diagnostic monitoring enclosures.
Strategic Procurement Insight: Global purchasers can dramatically lower their Total Cost of Ownership (TCO) by converting multi-component assemblies (screw + external O-ring + flat washer) into a single unified countersunk sealing fastener. This cuts assembly line labor steps by 65%, eliminates missing-washer human errors, and prevents over-compressed seal blowouts.
From vulcanized rubber-to-metal bonding chemistry to automated robotic feeder integration, fastener engineering is undergoing rapid modernization to keep pace with Industry 4.0 assembly lines.
Rather than relying solely on mechanically retained loose O-rings, cutting-edge fasteners feature molecularly vulcanized elastomers bonded directly to the underhead groove. This eliminates seal fallout during automated high-speed vibratory bowl feeding and robotic vacuum pick-and-place cycles.
Combining hermetic under-head O-ring sealing with 360° anaerobic micro-encapsulated threadlocking patches (e.g., DIN 267-27 / 3M Scotch-Grip). This creates a dual-defense system: preventing fluid migration at the head while permanently locking against dynamic harmonic vibration.
Aerospace and high-performance racing applications increasingly mandate Grade 5 (Ti-6Al-4V) titanium countersunk sealing screws. Offering a 45% weight reduction compared to steel alongside superior corrosion immunity, they provide critical gram-saving solutions for drone hulls and satellites.
From electrophoresis black finishes to precision locating spring ball plungers, explore complementary hardware designed for high-stress industrial and consumer electronics assemblies.
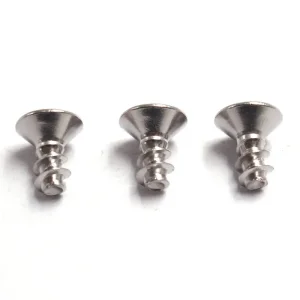
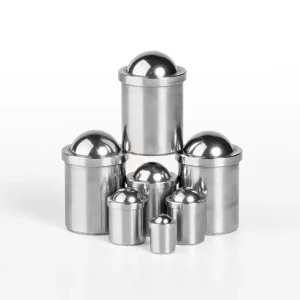
Authoritative answers on installation prep, torque requirements, material compatibility, and logistics from YH Fastener senior application engineers.
