Direct-to-plant procurement for high-vibration manufacturing, structural electronics, and high-tensile modular systems compliant with ANSI, ISO, and CSA standards.
Canadian advanced manufacturing demands mechanical fasteners capable of withstanding extreme thermal deltas, rigorous cyclic vibration, and complex cross-border regulatory frameworks.
Standard carbon steels experience severe Ductile-to-Brittle Transition (DBTT) under typical Canadian winter conditions (-40°C to -50°C). Our engineered alloy and cold-forged fasteners undergo controlled tempering and micro-alloying to guarantee Charpy V-notch impact toughness under continuous sub-zero shock loading.
Canada operates as an integrated hybrid market bridging US Customary (Imperial ANSI/ASME B18.6.3) threads for cross-border machinery and Metric (ISO 7045, DIN 7985) architectures for green-tech and European-spec transit equipment. We manufacture parallel production lines covering both threads seamlessly.
Serving Tier-1 and Tier-2 automotive clusters spanning the Windsor-Quebec corridor requires strict adherence to IATF 16949 standards, full Level 3 PPAP documentation, IMDS registration, and specialized multi-layer micro-zinc alloy plating exceeding 1,000 hours of neutral salt spray without white corrosion.
Cryogenic Ductility Baseline
Hours Salt Spray Resistance (ASTM B117)
Precision Cold-Forming Tolerance
Optoelectronic Dimension Screening
Modern industrial machinery cannot tolerate bolt loosening, hydrogen embrittlement, or premature galvanic oxidation. Our multi-stage process mitigates systematic joint failure points.
High-strength screws (Property Class 8.8, 10.9, 12.9 / Grade 5 & 8) subjected to acid pickling and electrolytic plating risk catastrophic brittle failure due to atomic hydrogen absorption. We utilize advanced mechanical finishing and mandatory computer-monitored de-embrittlement baking at 200°C–230°C within 4 hours of plating, verified through sustained load stress testing under ASTM F606 specifications.
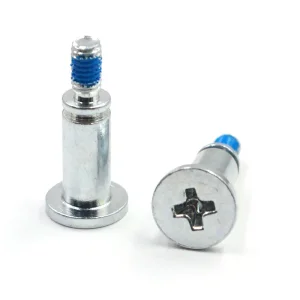
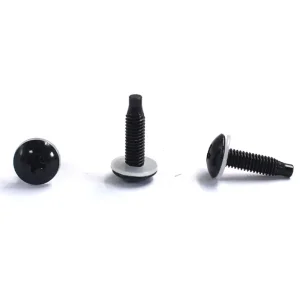
Dynamic cyclic transverse vibration is the leading cause of bolt self-loosening in transport and heavy equipment. Our locking mechanisms encompass integrated tooth washers (SEMS), engineered nylon patch polymers (360° or 180° radial deposit), and proprietary micro-encapsulated anaerobic adhesives (DIN 267-27) that activate upon torque application to form an absolute vibration barrier.
| Mechanical Property | Canadian Standard Reference | YH Fastener Manufacturing Capability | Operational Advantage |
|---|---|---|---|
| Tensile Strength | ASTM A307, SAE J429, ISO 898-1 | Class 4.8 to 12.9; Gr. 2 to Gr. 8 (Up to 1,220 MPa) | Zero necking under high dynamic tension and load peaks |
| Low-Temp Toughness | CSA W59, ASTM A320 L7/L7M | Impact verified down to -50°C (Charpy V-Notch > 27J) | Guaranteed survival during deep Canadian arctic operations |
| Corrosion Resistance | ASTM B117, ISO 9227 | Zinc-Nickel, Delta-Protekt, Multi-layer Dacromet | Protection against de-icing salts (MgCl₂, CaCl₂) on roads |
| Thread Precision | ASME B1.1 (2A/3A), ISO 965-2 (6g/6h) | Precision thread rolling post heat-treat option | Eliminates galling in automated robotic high-speed screwdriving |
Deploying precision fasteners across Ontario, Quebec, Alberta, and British Columbia's core manufacturing sectors.
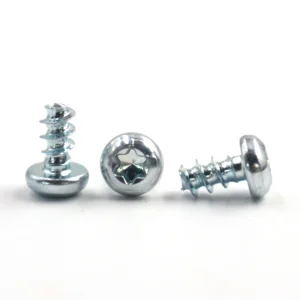
From battery pack chassis enclosures to powertrain subframes in Windsor, Oakville, and Oshawa. Our SEMS and PT thread-forming screws provide EMI shielding continuity, high strip-to-drive torque margins in plastics, and strict IATF 16949 traceable lot integrity.
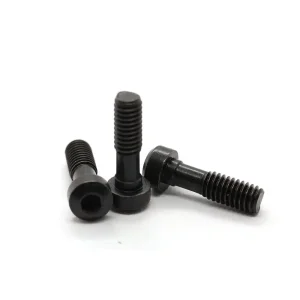
Serving Greater Montreal’s aviation supply cluster and mass-transit OEMs. Shoulder screws with tight-tolerance ground journals serve as precision hinge points, while stainless steel 316 A4-80 fasteners eliminate galvanic interaction in lightweight aluminum carriages.
Heavy machinery operating in the oil sands of Fort McMurray and offshore terminals in Vancouver require fasteners with superior fatigue limits. High-strength alloy machine screws with specialized sealing under-head O-rings isolate threads from abrasive tailings and brine.
Procuring fasteners internationally requires ironclad supply assurance and documentation. YH Fastener operates three manufacturing plants with over 20,000 m² of specialized production floor space, backed by continuous multi-gate metallurgical validation.
Every production heat is mapped to raw wire coils. Full chemical spectroscopy and tensile stress reports accompany every export container landed at Canadian ports.
Strict prohibition of hexavalent chromium (Cr6+), lead, cadmium, and mercury in surface coatings, ensuring full Canadian Environmental Protection Act (CEPA) compliance.
High-speed multi-camera laser screening machines inspect thread pitch, drive concentricity, head dimensions, and burrs to guarantee seamless automated feeding.
Anticipating the technological transformation of assembly lines across North America through ongoing R&D investments.
Flow-drill and thread-forming self-piercing screws designed specifically for hybrid aluminum-to-ultra-high-strength-steel structural joints in next-gen EV platforms.
Integrated piezoelectric and thin-film passive surface sensors for live clamp-load telemetry in critical aerospace assemblies and mining infrastructure.
Implementation of hydrogen-reduced green wire rod to decrease the embedded carbon footprint of exported fastener lots by up to 60%, aligned with Canadian net-zero benchmarks.
High-performance, fluoropolymer-free chemical topcoats delivering tight torque-tension coefficients (µ = 0.10 - 0.15) while satisfying forthcoming global PFAS regulatory bans.
Detailed mechanical, logistical, and metallurgical answers for engineering and procurement professionals sourcing for Canada.
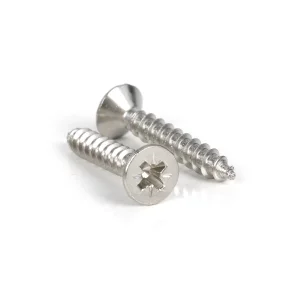
Browse our core cold-headed, thread-rolled fasteners engineered for plastic, composite, sheet metal, and precision mechanical integrations.




Direct cold heading, rolling, plating, and testing lines. Share your 2D/3D mechanical drawings or CAD models for rapid DFM evaluation and commercial quotations from senior fastener engineers within 24 hours.
Send Inquiry Now