Meeting tight ASME/DIN/ISO tolerance thresholds for Boston's cutting-edge life sciences automation, subsea exploratory equipment, and Route 128 robotics clusters.
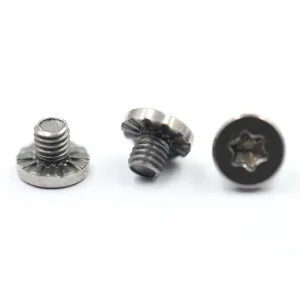
Engineered for high-torque assembly without drive slip in Waltham automated material-handling robotics.
Center security pin stops field tampering on sensitive server racks, radar arrays, and telecom nodes.
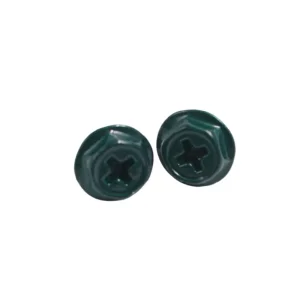
Compliant grounding terminal fastener with captive serrated washer for laboratory analytical gear.
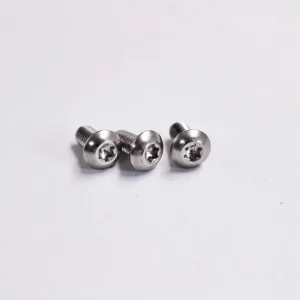
Ultra-smooth domed profile prevents snagging and maximizes space efficiency in compact bio-sensing devices.
From Cambridge biomedical incubators to Route 128 robotics centers and North Shore defense contractors, Greater Boston's advanced manufacturing demands extreme fastener reliability.
Waltham, Burlington, and Bedford host global leaders in autonomous mobile robots (AMRs), warehouse fulfillment bots, and quadruped platforms. These systems demand DIN 7985 and ISO 14581 machine screws treated with prevailing-torque nylon patches to prevent vibration back-off during continuous dynamic operation.
The biomedical capital of the world requires surgical robotics, microfluidic analyzers, and IVD hardware built with vacuum-melted 316L stainless steel screws. Passivated to ASTM A967 with zero trace contamination, our micro machine screws (down to M0.8) comply with sterile clinical environments.
Boston Harbor, Woods Hole, and the South Coast offshore wind corridor deploy oceanographic telemetry and subsea gliders. Fasteners in this zone must deliver guaranteed galvanic corrosion immunity through A4-70 (316) marine-grade stainless steel or specialized anti-galling fluoropolymer coatings.
Procurement teams at Boston-area original equipment manufacturers (OEMs) operate under severe quality mandates. Whether building robotic arms in Waltham, sequencing equipment in Cambridge, or avionics modules along the I-95 perimeter, fastener failure translates to unacceptable field recalls and device non-compliance. Our direct-from-source cold heading and thread-rolling plants operate under ISO 9001, ISO 14001, and IATF 16949 certification systems to ensure structural consistency across high-volume production lots.
We manufacture machine screws strictly compliant with ASME B18.6.3 (Slotted, Cross Recessed, and Torx machine screws), DIN 7985 (Pan Head), DIN 965 (Countersunk Flat Head), and ISO 7045/ISO 14581 standards. Metric thread engagements are machined and rolled to Class 6g and 4h/6h precision, while Unified National (UNC/UNF) threads are verified with calibrated GO/NOGO working ring gauges to Class 2A and 3A fit standards. Rolled threads retain uninterrupted grain flow around the root radius, resulting in a 20% to 30% higher cyclic fatigue threshold compared to cut threads.
| Material Specification | Tensile Strength (MPa) | Corrosion Resistance | Typical Boston OEM Application |
|---|---|---|---|
| 316 / A4-70 Marine Stainless | 700 - 800 MPa | 1,000+ hrs Salt Spray (ASTM B117) | Offshore acoustic sensors, Boston Harbor marine hardware |
| 304 / A2-70 Austenitic Stainless | 700 MPa | 500 hrs Salt Spray (Passivated) | Kendall Square laboratory automation, IVD clinical test devices |
| 10B21 Boron Steel (Class 8.8 / 10.9) | 800 - 1040 MPa | Zinc-Nickel / Black Oxide | High-shock robotics joints, warehouse automation AGV chassis |
| Titanium Gr 5 (Ti-6Al-4V) | 895 - 1000 MPa | Virtually Impervious / Non-Magnetic | MRI-compatible surgical robotic arms, MIT aero-space prototypes |
| Brass (C36000 / CZ121) | 340 - 450 MPa | Natural Anti-Galling & Conductive | High-frequency RF communications shielding, cleanroom grounding |
To prevent stress cracking in high-tensile carbon steel fasteners (hardness > 32 HRC), all electroplated lots undergo prompt de-embrittlement baking at 200°C–220°C within 4 hours of electroplating, sustained for a minimum of 8 to 24 hours per ASTM F1941. Stainless steel products are fully passivated to ASTM A967 (Nitric or Citric) to eliminate free iron embedded during heading, ensuring compliance with FDA biological contact guidelines and cleanroom particulate standards.
Boston high-tech startups and established industrial hardware giants frequently confront high domestic broker markups and inventory stockouts from local catalog distributors. By engaging directly with our multi-station cold heading and optical inspection facilities in Dongguan, New England buyers achieve significant supply chain benefits:
Discover how specialized machine screws are implemented across the prominent technological sectors of New England.
Precision micro flat-head Torx machine screws (M1.2–M2.5) installed inside multi-axis robotic wrists. Zero cam-out protects against particulate shedding in clean surgical fields.
Locations: Kendall Square, Longwood Medical Area, BedfordSems screws with captive dual spring-and-flat washers combined with pre-applied blue polyamide locking patches to withstand high shock loads and 24/7 continuous warehouse duty cycles.
Locations: North Shore industrial corridors, Route 128 Technology BeltUnder-head fluorosilicone sealing machine screws and passivated 316L hardware designed for oceanographic probes, deep-water buoys, and offshore wind sensor hubs.
Locations: Woods Hole, Boston Seaport, New Bedford PortFlanged grounding green-coated screws and vibration-resistant stainless fasteners utilized in modular battery packs, DC fast chargers, and smart electrical microgrid switchgear.
Locations: Somerville (Greentown Labs), Boston Tech IncubatorsStandard, miniature, and custom configured machine screws engineered for mission-critical mechanical fastening.
90-degree flat countersunk profile ensures smooth surface continuity in rackmount chassis and access doors.
Cold forged with deep drive recesses to allow high assembly seating torque without recess rounding.
Broad bearing flange face spreads clamp loads across sensitive sheet metal and non-metallic composites.
Molybdenum-bearing formulation provides superior resistance to pitting and crevice corrosion in salt spray.
Non-magnetic characteristics ideal for Mass Spectrometry devices, optical benches, and bio-sensors.
Designed for high-clamp civil, hydraulic, and structural mechanical assemblies requiring flat mounting.
Manufactured with tight concentricity tolerances under 0.03mm for precise alignment in optical stages.
Rugged, dependable metric and imperial standard threads designed for architectural enclosures and apparatus.
Technological innovation in cold heading, material sciences, and sorting systems redefining mechanical reliability.
Boston robotic assembly lines cannot tolerate jammed automatic screw-feeders. Every production lot runs through multi-camera laser and glass turntable inspection units, checking head height, drive concentricity, pitch pitch angle, and thread burrs at 1,200 parts/minute to secure <5 PPM quality rates.
Eliminating fluid chemical threadlockers on OEM shop floors, our automated pre-applied 360-degree nylon patches (DIN 267-28) and microencapsulated adhesives (DIN 267-27) provide reliable prevailing locking torque and thread sealing right out of the box.
For cryogenic laboratory equipment and high-temperature power electronics around Route 128, we supply machine screws cold formed and hot forged from Inconel 718, Hastelloy C-276, and Grade 5 Titanium, preserving mechanical tensile performance under severe operational stress.
Everything you need to know about specifications, certifications, tariffs, logistics, and quality assurance.
For urgent engineering builds, pre-production prototyping, and fast-turn production runs, we ship via DHL, FedEx, or UPS Priority direct to Logan International Airport (BOS), clearing customs and arriving at your Massachusetts facility in 3 to 5 business days. For high-volume sea shipments, containerized cargo arrives through the Port of Boston (Conley Terminal) or Port of NY/NJ with inland transfer to Massachusetts within 22 to 28 days. Standard custom tooling and sample manufacture take 7 to 10 days, with mass production runs averaging 15 to 25 days depending on secondary coating specifications.
We work under both FOB, CIF, and DDP (Delivered Duty Paid) terms depending on your procurement structure. Under DDP terms, our logistics partners manage all U.S. Customs clearance, HTS code classifications (e.g., Heading 7318 for threaded steel screws), Section 301 tariffs, and local harbor maintenance fees—delivering shipments straight to your dock in Boston, Cambridge, or Waltham without unexpected import surcharges.
Yes. Operating under our certified IATF 16949 and ISO 9001 systems, we routinely deliver comprehensive Production Part Approval Process (PPAP) Level 3 packages for automotive, industrial robotics, and medical device hardware accounts. This documentation includes Process FMEA, Control Plans, Gage R&R studies, Material Certifications (EN 10204 3.1), Salt Spray Test Validation (ASTM B117), and full 100% Dimensional First Article Inspection Reports (FAIR) performed on optical CMM equipment.
Hydrogen embrittlement represents a serious threat in case-hardened carbon steel and alloy steel screws with core hardness above 32 HRC (Class 8.8, 10.9, 12.9) exposed to acid pickling and electroplating. To eliminate this risk, our facility mandates an immediate de-embrittlement thermal bake within 4 hours of plating, held between 200°C and 220°C for 8 to 24 hours per ASTM F1941 / ISO 9588. Alternatively, we supply non-electrolytic zinc flake coatings (such as Geomet or Magni) which involve zero acid baths and zero hydrogen exposure.
For standard catalog items and standard metric/ASME dies, MOQs start as low as 5,000 to 10,000 pieces. For completely custom parts requiring custom-machined cold-heading dies, shoulder geometries, or captive washer combinations, our baseline production run typically begins at 20,000 to 50,000 pieces. However, for development programs across Boston tech incubators, we support initial pilot batches and sample runs (500–2,000 units) to accelerate dynamic testing prior to mass release.
