
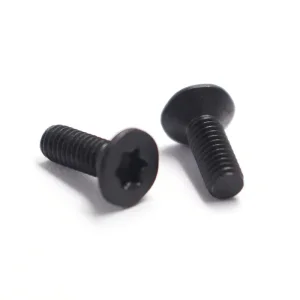
Precision-engineered indexable insert clamping fasteners for high-speed CNC milling, turning, and aerospace tooling. Direct-from-factory cold heading and thread-rolling serving Baden-Württemberg, Bavaria, and North Rhine-Westphalia tooling hubs.
Ultra-tight concentricity, Grade 12.9 high-tensile alloy options, and corrosion-resistant coatings specifically configured for indexable insert seats and precision assemblies.
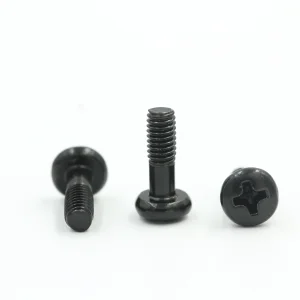


Meeting the extreme clamping requirements of Industry 4.0 machining centers across Germany's advanced automotive, mechanical engineering, and aerospace sectors.
German CNC milling centers run high-speed spindle operations (15,000 to 24,000+ RPM) where cutting inserts endure cyclical high-frequency shear. Our carbide insert screws utilize precision-rolled micro-threads (class 6g/4h) with controlled root radii to eliminate fatigue failure and premature loosening under continuous chip-load shocks.
Indexable toolholders demand precise seating. Using cold-heading dies calibrated for Torx and Torx Plus recess drive systems, our screws ensure radial torque transfer without cam-out damage. This enables toolmakers in regions like Stuttgart and Nuremberg to guarantee reproducible torque tightening tolerances within ±0.05 Nm.
Manufactured from premium SCM435, 42CrMo4, and custom alloy tool steel. Vacuum batch heat treatment controls hardness uniformly within 40–45 HRC (or ISO class 12.9 specification), maintaining core ductile toughness while preventing head shearing when securing solid cemented carbide or ceramic inserts.
| Parameter | German Industry Standard (VDI / DIN) | YH Precision Manufacturing Benchmark |
|---|---|---|
| Concentricity / TIR | ≤ 0.05 mm under-head to thread | ≤ 0.015 mm via multi-stage cold forging & optical sorting |
| Thread Profile Accuracy | DIN 13-1 Metric Fine Thread | Controlled root radius to reduce notch stress concentrations by 38% |
| Surface Coatings | Black Oxide, TiN, DLC, Phosphate | Molybdenum Disulfide (MoS2) dry film + Cr-free Dacromet coatings |
| Traceability & Compliance | EN 10204 3.1 Certification | Full lot heat-treatment charting, spectral material composition verified |
Combining world-class production capacity with German environmental standards, customs compliance, and dedicated engineering consultation.
Equipped with 300+ sets of multi-station high-speed headers and optical sorting lines capable of checking pitch diameter, head angle, and drive depth at rates exceeding 800 ppm. This eliminates line halts in automated robotic tool clamping systems.
Every shipment bound for Frankfurt, Hamburg, or Munich is certified compliant with EU REACH regulation (EC 1907/2006) and RoHS directives. Hexavalent chromium-free electroplating and zinc-nickel passivations withstand 720+ hours of neutral salt spray tests.
Mitigate geopolitical and supply chain volatility. Our dedicated export team manages seamless DDP/FOB workflows with buffered consignment warehousing options, reducing tooling component acquisition costs by up to 35% without sacrificing DIN-level quality.
Verification of head taper angle (60°/90°), pitch tolerance, and clearance under head per VDI 3324 standards.
Rapid cold-heading die production and pilot batch sampling with Cpk statistical process reports within 7–10 days.
High-resolution laser sorting verifies 360° concentricity, head dimensions, and thread integrity before packaging.
Traceable sea/air logistics direct to your production centers or distribution hubs across Germany with EN 10204 3.1 documentation.
Explore our complete catalog of industrial-grade machine, socket head, sealing, and anti-loosening fasteners engineered for European mechanical assemblies.

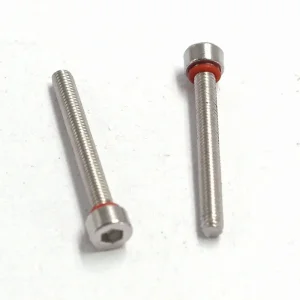
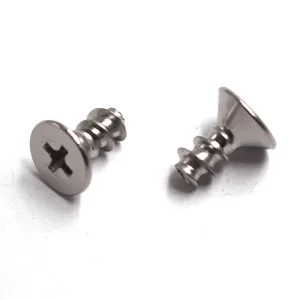
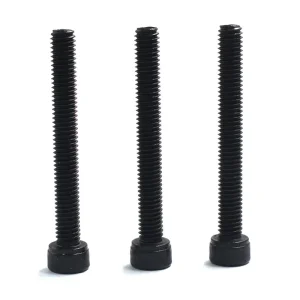
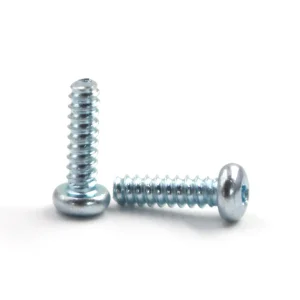
Specific guidance on tolerances, material certification, Torx specifications, and export logistics for German procurement teams.