
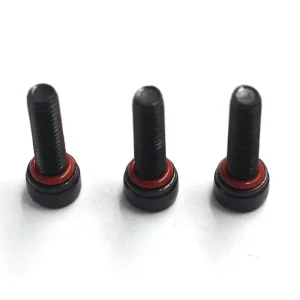
Explore engineered cold-forged screws, thread-forming solutions, and waterproof assemblies manufactured alongside perfectly calibrated driver bit configurations.


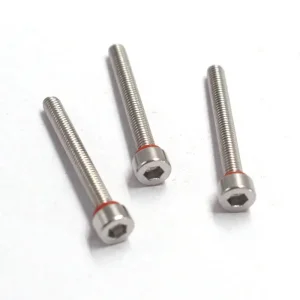
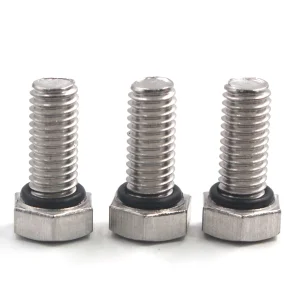
Global manufacturing across automotive electrification, telecommunications, and industrial automation has evolved beyond purchasing disconnected commodity hardware. The demand for "wholesale fastener matching wrench factories" represents an engineering shift: sourcing integrated fastener-tool sets engineered from matched tooling to eradicate cam-out, radial stress failures, and assembly rework.
When high-tensile internal drive screws (Hex socket DIN 912 / ISO 4762 or Torx ISO 10664) are paired with off-the-shelf wrenches from secondary sources, clearance tolerance stack-up leads to Hertzian contact stress concentrations. Sourcing matched wrenches forged to exact micro-recess dimensions achieves up to 98.4% surface engagement, nullifying cam-out and preserving anti-corrosion barrier coatings during final torquing.
A persistent cause of manufacturing downtime is galling between driver bits and fastener sockets. As an integrated manufacturer, Yu-Huang Fasteners designs paired sets where companion L-keys (hardened to HRC 58-62 via vacuum carburizing) maintain precise yield properties relative to fastener core hardness (Class 8.8, 10.9, 12.9, or austenitic stainless 304/316), preventing driver tip fracturing or socket wall reaming.
For consumer electronics, medical diagnostics, and ready-to-assemble (RTA) mechanical modules, OEMs require companion custom wrenches packed within identical lot-traceable packaging. By coordinating screw manufacturing and wrench cold-drawing under one factory umbrella, assembly plants reduce procurement line items, eliminate vendor finger-pointing, and streamline automated kitting processes.
The Pearl River Delta manufacturing corridor represents the pinnacle of high-volume fastener cold-heading and specialized drive wrench stamping. Yu-Huang Electronics Dongguan Co., Ltd. leverages this ecosystem to compress development, sample validation, and mass delivery timelines.
By producing heading dies, thread-rolling plates, and matching hex/torx punch pins in-house on high-speed CNC EDM centers, tool wear is continually monitored. When an M3 socket head or tamper-proof security pin is modified, the corresponding L-wrench bending die and extrusion broach are updated synchronously, assuring micrometer-level fit consistency.
With primary manufacturing centered in Dongguan and extended production hubs in Shaoguan and Wuhan, our manufacturing floor houses over 400 multi-station cold-heading units and automated thread rollers. This multi-regional operational redundancy insulates international supply chains against localized disruptions and capacity bottlenecks.
Every fastener and tool lot undergoes raw-wire spectroscopic metallurgical validation, continuous mesh-belt furnace heat treatment monitoring, optical sorting for thread geometry (pitch diameter, runout, drive recess depth), and 720-hour salt spray chambers (ASTM B117) for anti-corrosion finishes including trivalent zinc, Dacromet, and black oxide.
| Dimensional & Mechanical Parameter | Fastener Engineering Scope | Matching Wrench Engineering Scope | Inspection Standard |
|---|---|---|---|
| Nominal Size Range | M0.8 – M12 (#00 to 1/2" dia) | 0.7mm – 10.0mm (0.028" – 3/8" AF) | Calibrated Optical Projector / Micrometer |
| Drive Form Geometry | Hex Socket, Torx (6-Lobe), Security Pin-Hex, Tamper-Torx, Triangular, PT Thread | Standard L-Key, Short-Arm, Long-Arm, Ball-End, Flag-Handle, Keyring Torx | ISO 10664, DIN 911 / ISO 2936 Recess Gaging |
| Metallurgical Alloys | 1018A, 1022A, 10B21, SCM435, Stainless Steel 302, 304, 316, Brass H62 | Chrome Vanadium (Cr-V 6150), S2 Tool Steel, Carbon Steel 45#, 40Cr | Spectrometric Chemical Analysis |
| Core Hardness Rating | HV 240 – HV 450 (Class 4.8 to 12.9 equivalents) | HRC 50 – 54 (Standard Carbon), HRC 58 – 62 (Industrial S2) | Rockwell / Micro-Vickers Hardness (ASTM E18) |
| Surface Protection | Zinc + Cr3+ Passivation, Black Zinc, Ni-Plate, Sealing O-Rings, Nylon Patching | Bright Chrome, Black Oxide, Manganese Phosphate, Satin Nickel, Color Dip | Neutral Salt Spray ASTM B117 (24h to 1000h) |
Different engineering sectors impose specific constraints on thread engagement, head clearance, installation speed, and field maintenance. Here is how matched screw and wrench manufacturing solves critical edge cases.
Sealing screws with under-head elastomer O-rings (as featured in our waterproof lineup) must be seated with precise angular velocity and torque limits to prevent rubber extrusion while maintaining IP67/IP68 sealing. Providing customized torque-limiting L-wrenches or designated Torx Plus drivers directly to EV assembly sub-contractors guarantees identical seating pressure during field repairs.
Our PT thread-forming screws utilize optimized 30° flank angles to reduce radial hoop stress in polycarbonate and ABS casings. Matching these precision micro-fasteners with ultra-short-arm hex or mini Torx keys allows service technicians to execute maintenance inside cramped telecom, optical router, and avionics enclosures where standard pneumatic tools cannot access.
Outdoor kiosks, railway signage, and utility meters require tamper-proof security fasteners (triangular recess, pin-in-hex, or pin-in-Torx). Because security bits are non-standard by design, purchasing matched wrenches from the primary fastener factory ensures security keys are distributed strictly to certified service agents, reducing unauthorized field tampering.
Toolholders and indexing plates require carbide insert screws and spring plungers that endure continuous high-frequency vibration and coolant immersion. Paired heavy-duty Cr-V hex keys with chamfered lead-in tips permit rapid insert swaps without chipping internal socket walls, preserving concentricity in precision multi-axis milling heads.
Procurement teams managing multi-million-dollar bills of materials (BOMs) evaluate fastener manufacturers on total cost of ownership (TCO), documentation traceability, and compliance frameworks rather than raw unit price alone.
Tier-1 procurement mandates full Level-3 Production Part Approval Process (PPAP) submissions, including initial sample inspection reports (ISIR), IMDS chemical filings, and Mill Test Certificates (MTCs) conforming to EN 10204 3.1. Yu-Huang provides lot-tracked heat numbers verifying steel purity and non-conflict mineral adherence for every container shipped.
Splitting fastener orders to factory A and wrenches to factory B incurs double inspection fees, twin shipping bills of lading, and custom clearing complexities. Consolidating screws, spring plungers, captive fasteners, and mating wrenches into a single wholesale supplier drops administrative procurement overhead by 18% to 27% annually.
Global compliance frameworks including EU RoHS, REACH, and California Proposition 65 require non-hexavalent finishes. Yu-Huang utilizes advanced trivalent zinc plating, multi-color electrophoretic deposition, and Teflon-based thread friction-modifier coatings that resist extreme temperature fluctuations without off-gassing hazardous volatiles.
Engineered DIN/ISO standard and bespoke fasteners manufactured for high-reliability electronics, mechanical frames, and robotics enclosures.


Clear, authoritative technical answers regarding tolerances, material testing, anti-loosening technologies, and international wholesale export logistics.