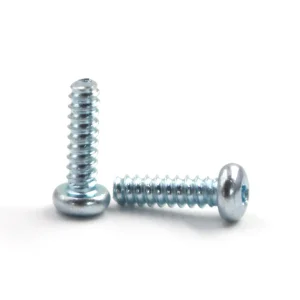
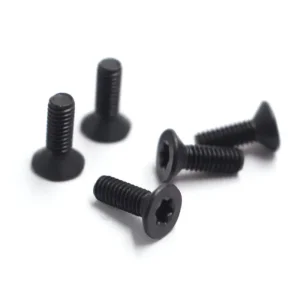
Engineered to rigorous DIN, ISO, ANSI, and JIS metric standard tolerances. Multi-station formed with unbroken metallurgical grain flow for superior shear, fatigue, and torsional performance.


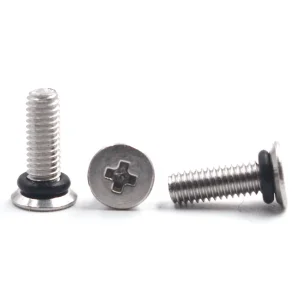
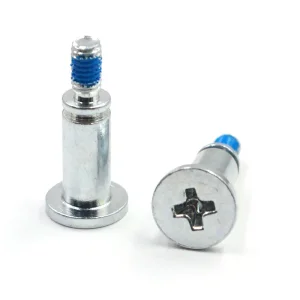
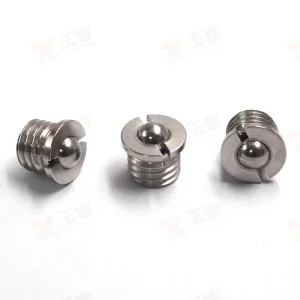
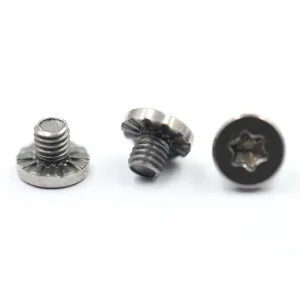
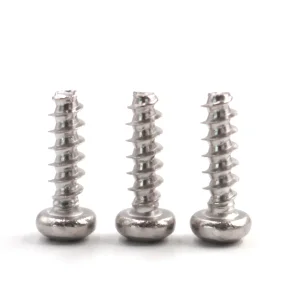
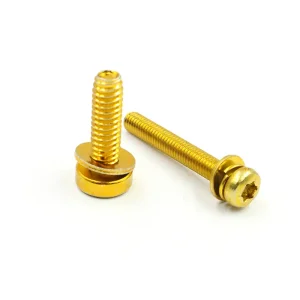
Metric machine-thread fasteners operate under severe mechanical, thermal, and chemical stress regimes. Our ODM engineering protocols tailor thread profiles (ISO 965-1 Class 6g/6H), micro-grain metallurgy, and surface conversion layers to specific operational demands.
Structural reliability within lithium-ion battery enclosures, inverter cooling plates, and drive units requiring IP68/IP69K sealing screws, Class 10.9/12.9 high-tensile steels, and pre-applied micro-encapsulated thread lockers.
Ultra-miniature metric machine screws (M0.6 to M2.0) engineered for compact smartphones, VR optics, camera gimbals, and 5G transceiver heat sinks requiring non-magnetic austenitic stainless (SUS304/SUS316) and zero-burr drives.
Kinematic alignment and recurring cyclic vibration protection using case-hardened shoulder screws, precision captive washers (SEMS), and slotted ball plungers engineered for index detents in high-cycle automated tooling.
High-yield outdoor mechanical fastening exposed to continuous UV degradation, atmospheric chlorides, and sustained wind-shear loads. Featuring premium stainless alloys and structural zinc flake barrier coatings.
Spanning a tri-facility production network across Dongguan (Advanced R&D and High-Precision Micro-Heading), Shaoguan (Heavy Forming & Carbon Steels), and Wuhan (Inland Industrial Cluster Fulfillment), YH Fastener delivers vertical integration without intermediary reliance.
Multi-die cold heading machines paired with computerized wire feeding preserve crystalline grain flow, yielding 25% higher shear and fatigue resistance compared to turned or cut threads. High-speed planetary and flat die rollers sustain ISO 965 tolerance windows across million-unit lot production.
Atmosphere-controlled continuous furnace lines prevent surface decarburization and quench micro-cracking. Automated carbon potential sensors maintain carbon saturation within ±0.02%, systematically achieving specified Property Classes 4.8, 6.8, 8.8, 10.9, and 12.9 with predictable Vickers (HV) and Rockwell (HRC) distributions.
Every critical batch passes multi-camera optical rotary glass disc sorting systems. AI computer vision models evaluate major diameter, pitch, flank angle, drive depth, plating defects, and thread damage at speeds exceeding 800 parts per minute, ensuring zero assembly line stoppages for tier-1 automated feeder bowls.
As automated robotic assembly lines demand lower insertion torques and higher joint security, YH Fastener advances its R&D across lightweight alloys, tribological nano-coatings, and structural intelligence.
Addressing aggressive weight-shedding mandates in aerospace robotics and premium electric vehicle battery systems. Continuous expansion into cold-headable Titanium Ti-6Al-4V, high-strength 7075 aluminum, and lightweight magnesium fasteners delivering 40% to 60% mass savings over steel with superior specific tensile strength.
Replacing traditional wet thread lubricants with dry, non-reactive solid lubricating thin films (PTFE, MoS2, and diamond-like carbon DLC). These coatings guarantee consistent coefficient of friction (μ = 0.10 - 0.14) over repeated tightening cycles without shedding particulate debris into cleanrooms.
Early-stage engineering protocols integrating micro-transponders and strain-sensitive piezoelectric crystals inside the fastener shank. Enables real-time ultrasonic clamp load verification and asset tracking throughout the product lifecycle, vital for automated warranty tracking and offshore wind turbines.
International manufacturing groups prioritize supply security, regulatory transparency, and total cost of ownership (TCO) over initial unit cost alone. Here is how our engineering-first sales infrastructure mitigates cross-border procurement vulnerabilities.
Every shipment is accompanied by comprehensive quality and material provenance documentation: EN 10204 3.1 chemical & physical mill certificates, RoHS Directive (EU) 2015/863, REACH SVHC declarations, and conflict minerals reporting (CMRT).
Production Part Approval Process (PPAP) including Process FMEA, Control Plans, Gage R&R repeatability studies, and Dimensional Results across multiple cavities. This rigor translates directly into aerospace, medical hardware, and industrial equipment confidence.
Eliminate multiple micro-suppliers by consolidating machine screws, thread-forming fasteners, captive SEMS, positioning spring plungers, and companion Torx/Hex wrenches under one accountable roof with EDI connection and Vendor-Managed Inventory (VMI) support.
| Engineering Parameter | Standard Specification Range | Factory Capability Limit | Applicable Standards & Quality Codes |
|---|---|---|---|
| Nominal Thread Diameter | M1.0 to M12.0 (Metric Machine Coarse / Fine) | M0.6 (Ultra-Micro) to M20.0 | ISO 261, ISO 965-1, DIN 13, ASME B1.13M |
| Mechanical Property Classes | Class 4.8, 6.8, 8.8, 10.9, 12.9 (Alloy/Carbon) | A2-70, A4-80 (Austenitic), Brass CW614N | ISO 898-1, ISO 3506-1, DIN 267 |
| Thread Fit & Pitch Tolerance | Class 6g (External Threads), Class 6H (Internal) | Class 4h / 5h High Precision Aerospace Fit | ISO 965-2, Go/No-Go Gauge Verification |
| Drive Recess Geometries | Torx (6-Lobe), Phillips (Type H), Slotted, Hex Socket | Torx Plus®, Tamper-Proof Pin-in, Triangular | ISO 10664, DIN 7985, ISO 7045, ISO 14583 |
| Surface Protection & Salt Spray | Trivalent Zinc (Cr3+), Nickel, Black Oxide (96-240h) | Zinc-Nickel, Geomet®, Dacromet® (1000h - 1500h) | ASTM B117, ISO 9227, DIN 50021 |
| Locking & Hermetic Additions | Nylon Patch (180°/360°), Chemical Threadlock Microcaps | Captive EPDM/Silicone O-Rings, Multi-Washer SEMS | DIN 267-27, DIN 267-28, IFI 124 / 524 |
Direct answers to technical queries regarding cold-heading tolerances, thread fitment, anti-loosening mechanisms, and factory direct customization protocols.
Cold thread rolling is a chipless forming process where hardened steel dies plastically deform the blank shank. This cold working burnishes root radii and forces metallurgical grain lines to flow continuously along the thread contour rather than severing them. The outcome is up to a 20-30% increase in shear strength, exceptional surface hardness at the flanks, improved fatigue endurance, and lower micro-roughness (Ra < 0.4 μm).
Electroplating high-strength carbon/alloy steels (hardness exceeding 320 HV / 32 HRC) releases atomic hydrogen that can migrate to grain boundaries and cause sudden delayed failure under preload. We strictly enforce immediate de-hydrogenation baking (de-embrittlement) at 200°C to 220°C for a minimum of 4 to 8 hours within two hours post-electroplating, verified via sustained load testing per ISO 15330.
Standard metric machine screws possess a constant round cylindrical shank conforming to ISO 965 and require pre-tapped metric holes or companion nuts. Thread-forming (PT or trilobular) screws feature a cross-section with an engineered 30° flank angle that displaces and rolls mating internal threads into plastic or light sheet metal substrates without pre-tapping, eliminating chips and providing superior strip-to-drive torque ratios.
Our OEM sealing screws feature a precision cold-formed or CNC-undercut groove under the head bearing surface. When torqued into the mating component, an engineered elastomeric O-ring (NBR, Silicone, or Viton/FKM) is compressed within the annular cavity. This stops lateral escape, delivering an IP67/IP68 hermetic seal against fluids, moisture, and gases without extruding or degrading under dynamic vibration.
Yes. Our engineering division in Dongguan reviews 3D models (STEP, IGES, SolidWorks) along with 2D drawings defining critical tolerances, GD&T, surface treatment, and torque parameters. We evaluate manufacturability (DFM), design cold-heading tooling and progressive dies in-house, produce rapid prototype lots, and provide full FAI (First Article Inspection) and PPAP Level 3 documentation prior to mass run releases.
We offer three main anti-loosening systems depending on service conditions: 1) Polyamide/Nylon patches applied over a 90°-360° thread arc for reusable prevailing torque; 2) Pre-applied micro-encapsulated anaerobic chemical adhesives (e.g., 3M, precote, Loctite) that cure upon engagement for permanent thread locking; 3) Mechanical SEMS combination screws with captive serrated, conical, or wave lock washers that maintain joint preload under harmonic shocks.
From micro-electronics Torx-drive screws to structural machine bolts and PCB standoff fasteners. Engineered and tested under our unified ISO/IATF quality management framework.