Explore our specialized range of custom cold-headed pan head self-tapping and tamper-proof machine screws optimized for high-vibration assemblies, electronics enclosures, and automotive housings.

An in-depth analysis of fastener kinematics, flank angles, clamp force retention, and anti-tamper head geometry for modern industrial design engineers.
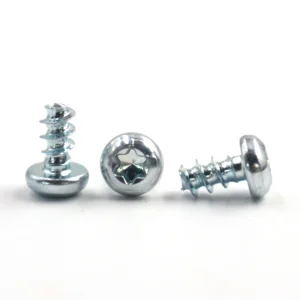
The pan head profile features a flat bearing surface with a slightly rounded outer periphery, engineered according to DIN 7981, ISO 7049, and ASME B18.6.3 standards. Unlike countersunk screws that induce significant hoop stress into the mating plastic or sheet substrate, the pan head applies orthogonal compressive force directly to the joint surface.
This uniform bearing pressure dramatically minimizes plastic cold-flow and sheet metal distortion under high torque, providing an optimal load distribution ratio that maintains joint clamp load even through extreme thermal expansion cycles (-40°C to +125°C).
A high-performance security screw requires thread geometry tailored specifically to the host material's tensile modulus and flow behavior. Our automated thread-rolling lines form cold-worked, continuous grain-flow thread paths:
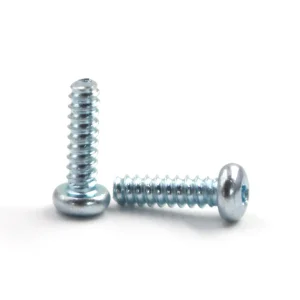
PT 30° Flank Threads: Standard self-tapping fasteners employ a 60° thread angle which induces excessive radial bursting stress. Our engineered PT thread utilizes a narrowed 30° flank angle, reducing radial force while dramatically increasing axial shear engagement.
Field tampering, warranty fraud, and internal sabotage represent millions in operational risk. We manufacture tamper-resistant recesses requiring specialized engagement bits not available in conventional retail toolsets:
Torx TR (Tamper-Resistant Pin-in-Torx): Incorporates a precision central solid post preventing standard hex or standard Torx bit entry, while retaining the outstanding cam-out resistance and torque-transfer efficiency of six-lobe geometry.
Comprehensive metallurgical mapping, surface electrochemistry, and functional properties across our custom pan head security fastener portfolio.
| Material Grade | Tensile Strength (MPa) | Core Hardness | Surface Treatment / Plating Options | Corrosion Resistance (Salt Spray) | Primary Industrial Sector |
|---|---|---|---|---|---|
| Austenitic Stainless 304 (A2-70) | 700 – 800 | HV 190 – 250 | Passivation, Electro-polishing, Black Oxide | 400 – 600 Hours (ASTM B117) | Consumer Electronics, Smart Water Meters, Outdoor Enclosures |
| Marine Stainless 316 (A4-80) | 800 – 900 | HV 210 – 280 | Ultrasonic Passivation, Teflon (PTFE) Coating | 1,000 – 1,500 Hours (Salt Spray) | EV Charging Stations, Marine Navigational Hubs, Chemical Plants |
| Case-Hardened Carbon Steel (1022A) | 900 – 1,050 | HRC 32 – 40 (Case: HRC 55+) | Eco-Zinc (Cr3+), Zinc-Nickel Alloy Plating, Geomet | 240 – 720 Hours (Controlled Deposit) | Automotive Sheet Metal, Plastic Assembly, Industrial Machinery |
| High-Alloy Alloy Steel (SCM435) | 1,040 – 1,220 | HRC 38 – 45 | Black Zinc, Phosphating, Dacromet Coating | 500 – 1,000 Hours (Heavy Anti-Rust) | Rail Transit Bogies, Renewable Energy Inverter Casings |
| Specialty Brass / Cu-Alloy (C3604) | 450 – 550 | HRB 65 – 80 | Nickel Flash, Tin Plating, Gold Flash | 120 – 240 Hours | Spark-Free Utility Infrastructure, RF Shielded Compartments |
In automated production lines, the window between seating torque (Ts) and stripping torque (Tl) must be engineered with a minimum ratio of 1:3. Our cold-forming tooling produces precision thread leads with razor-sharp crests and generous root radii that slash insertion torque by up to 35% while augmenting strip-out torque.
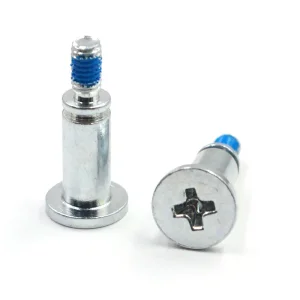
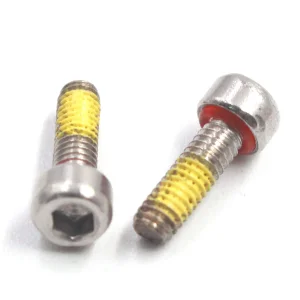
For applications subject to continuous operational harmonic vibration, we integrate micro-encapsulated chemical threadlockers (DIN 267-27) or pre-applied 360° blue nylon locking patches (DIN 267-28), creating an impenetrable prevailing torque seal that stops vibratory loosening permanently.
High-strength carbon steel self-tapping fasteners (hardness > HRC 32) are extremely vulnerable to Hydrogen Embrittlement (HE) during electroplating and pickling baths.
Our ISO 14001 electroplating facility executes an automatic 4-to-8 hour de-hydrogenation baking process at 200°C–220°C within two hours post-pickling. Furthermore, for mission-critical automotive projects, we provide non-electrolytic Zinc Flake coatings (Geomet / Magni / Delta-Protekt) that eradicate acid contact completely, guaranteeing zero risk of delayed brittle fractures under preload.
Why Tier-1 hardware developers and global OEMs are prioritizing physical fastener security across distributed infrastructure, edge computing, and mobility.
In modern consumer electronics and high-value industrial machinery, unauthorized consumer teardowns and third-party repair intrusions void warranties, cost billions in unverified claims, and expose proprietary PCB architectures to intellectual property piracy.
Custom security pan head fasteners act as an unequivocal physical tamper barrier. By controlling driver distribution to authorized service technician centers only, manufacturers enforce warranty integrity and retain total control over post-sale hardware servicing and diagnostics.
As cities roll out smart electric meters, 5G small-cell base stations, smart lighting, and decentralized EV charging grids, sensitive electrical hardware is exposed to public vandalism, component theft, and hazardous live-voltage tampering.
Municipal regulatory frameworks now mandate tamper-proof locking hardware for all exterior service compartments. Our corrosion-resistant stainless steel 316 pin-drive pan head fasteners withstand decades of exposure while preventing unauthorized bypass or electrical tap theft.
International safety certification directives (including UL 60950, IEC 62368-1, and CE machinery directives) dictate that hazardous high-voltage power supplies and chemical battery modules must not be accessible via ordinary tools like flathead or cross screwdrivers.
Engineers utilize our tamper-resistant pan head self-tapping hardware to achieve instant compliance with international safety audit protocols without having to re-engineer expensive stamped chassis latches or exterior cover locksets.
Proven mechanical fastening performance across mission-critical aerospace, electric mobility, medical diagnostic, and telecom systems.
Operating Environment: Severe outdoor UV, driving monsoon rains, thermal swings from -30°C to +75°C, high magnetic fields, and intense mechanical vibration.
Engineering Solution: Custom Pan Washer Head Self-Tapping Security Screws fabricated in Passivated Stainless Steel 316. Coupled with molded silicone under-head O-rings to deliver verified IP67 moisture impermeability. Pin-Torx drives eliminate sabotage attempts on high-power 800V DC switching modules.
Operating Environment: Rooftop and tower-mounted aluminum die-cast radomes requiring zero RF electromagnetic interference and decades of corrosion resistance.
Engineering Solution: Trilobular thread-rolling pan head fasteners forming zero-clearance mating threads in die-cast aluminum without generating conductive metal debris. Pre-applied dry threadlocking microcapsules ensure 100% clamping retention against severe wind vortex vibrations.
Operating Environment: Cleanroom enclosures subject to aggressive daily chemical sterilization (bleach, IPA, hydrogen peroxide vapor) requiring complete absence of particle contamination.
Engineering Solution: Non-magnetic Austenitic 316L pan head security screws with custom 5-lobe pentalobe pins. Cleaned via multi-stage ultrasonic degreasing in certified ISO Class 7 cleanrooms and vacuum-bagged for immediate medical chassis assembly.
Operating Environment: Highly distributed residential and commercial deployments vulnerable to magnetic tampering and bypass wire insertions.
Engineering Solution: Custom One-Way Pan Head Self-Tapping Screws with specialized anti-rotation serrations underneath the head. These screws can be torqued down rapidly during factory assembly, but the installation tool slips out during any unscrewing attempt, creating a permanent tamper-evident housing seal.
Operating Environment: Battery Management Systems (BMS) in hybrid and battery-electric vehicles subjected to continuous multiaxial road shock and high thermal cycling.
Engineering Solution: Carbon Steel PT-Thread Pan Head Screws with Zinc-Nickel black alloy electroplating (>1,000h salt spray without red rust). The custom PT 30° thread avoids cracking glass-filled polyamide battery frames, providing 4.5 Nm of strip resistance.
Operating Environment: Passenger cars, signal junction boxes, and operator console displays subject to strict vibration safety standard EN 61373 Cat 1 Class B.
Engineering Solution: High-strength Grade 10.9 SCM435 alloy steel pan head screws with custom security recesses and captive SEMS Belleville spring washers. The conical washer geometry maintains live clamp load despite bolt elongation under sustained dynamic shocks.
How our vertically integrated production base and regional supply cluster empower global OEMs with unprecedented speed, cost-efficiency, and scale.
Operating from the hardware manufacturing capital of Dongguan, China, Yu-Huang Electronics leverages an unparalleled supply chain radius. High-purity wire rod mills, specialized carbide heading die makers, automated vacuum heat-treatment furnaces, and environmental plating centers operate within a 30-minute logistics perimeter.
This concentrated ecosystem eliminates weeks of subcontracting freight time, shielding our buyers from global logistics disruptions while enabling ultra-responsive material sourcing across exotic alloys (Titanium, A286, Brass, Inconel).
Where traditional Western fastener houses quote 8 to 14 weeks just to construct heading dies for non-standard security drive recesses, our in-house CNC toolroom and Sodick EDM wire-cutting centers machine custom carbide punches within 48 to 72 hours.
OEM engineers can upload 3D CAD step files or 2D dimensioned drawings and receive functional first-article cold-headed samples within 7 business days, shortening new product introduction (NPI) cycles by up to 70%.
With over 20,000 m² across three manufacturing facilities (Dongguan HQ, Shaoguan, Wuhan), YH Fastener keeps every phase of production under our direct IATF 16949 audit trail:
Complete traceability, documentation transparency, and localized DDP logistics for Tier-1 supply chain procurement teams.
For our automotive, medical, and aerospace tier customers, we provide comprehensive documentation packages following the AIAG framework:
Our in-house QA laboratories are staffed by certified metallurgists and metrology engineers equipped with cutting-edge analytical hardware:
Exporting to over 60 countries across North America, the European Union, Southeast Asia, and South America, YH Fastener provides total logistics flexibility:
Anticipating the technological demands of autonomous systems, lightweight composites, and cyber-physical security.
The future of industrial assembly lies in digital traceability. YH Fastener is pioneering pan head security fasteners with ultra-compact laser-etched 2D DataMatrix codes and integrated passive NFC/RFID silicon microchips embedded directly within the drive cavity.
This enables automated robotic assembly arms to verify screw part numbers, exact metallurgical heat batches, and optimal factory tightening torques in real time, while recording lifecycle maintenance histories on immutable enterprise ledgers.
As electric aircraft (eVTOL) and high-density EV battery packs strive to shed every gram of weight without sacrificing structural clamp integrity, our R&D team is expanding cold-heading protocols for Grade 5 Titanium (Ti-6Al-4V) and Duplex 2205 Stainless Steel.
These advanced alloys deliver a 45% weight reduction compared to conventional steel while offering tensile strengths exceeding 950 MPa and virtually indefinite immunity to saltwater galvanic corrosion.
Transitioning beyond standard 2D dimensional sorting, our newest inspection lines integrate deep-learning convolutional neural networks (CNN). Multi-camera high-frame-rate systems evaluate micro-burrs in drive recesses, micro-cracks in thread crests, and plating voids at speeds exceeding 800 parts per minute.
This autonomous AI vision architecture enforces a true Zero-Defect (<1 PPM) standard, directly satisfying the hyper-strict requirements of automated robotic assembly lines.
Authoritative technical guidance addressing common engineering queries regarding thread selection, tooling life, and custom drive specifications.
Thread-forming screws (such as PT-thread or Taptite trilobular styles) displace and cold-flow the host material without cutting grain fibers or creating chips. This process work-hardens the internal thread profile, creating high prevailing torque and exceptional resistance to vibratory loosening. They are best suited for ductile plastics (ABS, Polycarbonate, Nylon) and thin ductile metals (aluminum, low-carbon steel).
Thread-cutting screws (such as Type F, Type 1, or Type 23) feature integrated cutting flutes and edges that cleanly remove material, creating sharp mating machine threads. They are mandatory in brittle materials such as cast zinc, magnesium alloys, and thermoset bakelites where thread-forming pressures would cause catastrophic boss cracking.
A pan head distributes tensile clamping load horizontally across its flat underside bearing area, whereas a countersunk head introduces wedging (hoop) stresses that push outward radially. In plastic boss structures or thin metal covers, countersunk screws frequently cause cosmetic crazing, edge splitting, and boss dilation under high seating torque.
Furthermore, a pan head allows for the integration of captive lock washers, Belleville discs, or elastomer O-rings directly underneath the bearing surface to achieve hermetic IP67/IP68 ingress seals. Its low-profile chamfered edge also prevents unauthorized gripping with locking pliers, maximizing physical security.
Fasteners with a core hardness exceeding HRC 32 or tensile strength >1000 MPa absorb atomic hydrogen during acid pickling and electrolytic plating. To eliminate this critical failure mode, we follow strict ASTM F1941 and ISO 9588 specifications:
1. Parts are immediately transferred to convective de-hydrogenation baking ovens within 1 to 2 hours of electroplating, baking at 200°C–220°C for a minimum of 4 to 8 hours.
2. For safety-critical automotive fasteners, we recommend non-electrolytic dip-spin zinc flake coatings (Geomet / Dacromet), which involve completely neutral chemical pre-cleaning and eliminate hydrogen evolution entirely.
3. Every heat-treated lot undergoes destructive pre-load testing under 80% yield stress for 48 hours to certify zero delayed fracture risk.
Yes. We regularly design and patent proprietary drive patterns (such as non-standard asymmetrical multilobes, dual-eccentric pin holes, and variable-angle keyways) for OEM customers. Under our non-disclosure agreement (NDA), we manufacture both the specialized cold-heading drive punches and the corresponding assembly driver bits / L-keys exclusively for your supply chain.
This ensures that no third party, unauthorized distributor, or counterfeiter can purchase matching tooling on the open market, creating a completely secure closed-loop hardware ecosystem.
For standard custom configurations (standard pan head with pin-Torx or security drives in carbon steel or 304 stainless), our typical production MOQ starts at 20,000 to 50,000 pieces depending on fastener length and wire diameter. For rapid prototyping and pilot builds, we offer expedited soft-tooling runs starting at 5,000 pieces.
Tooling design and first-article sample production typically require 7 to 10 working days. Full mass production batches are completed within 15 to 22 business days post-sample approval, supported by localized sea/air DDP shipping directly to your assembly plant.
Explore our extended catalog of industrial fasteners, featuring precision machine threads, non-standard metric dimensions, ultra-thin profiles, and specialized thumb screws.




Submit your 2D engineering drawings (PDF/DXF) or 3D CAD files (STEP/IGES). Our senior application engineers will analyze clamping mechanics, pitch ratios, surface finishing chemistry, and deliver a comprehensive DFM audit with quote within one business day.
