Engineered cold-formed fasteners with anti-loosening threads, specialized micro-coatings, and hermetic sealing for high-stress structural and electronic assemblies.

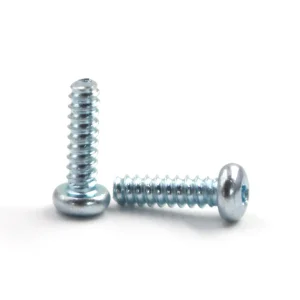



A rigorous review of thread geometry, fiber cleaving dynamics, rotational insertion resistance, and mechanical load transfer across natural grain matrices.
Unlike homogeneous isotropic substrates such as structural carbon steel or cast aluminum, structural timber is an orthotropic cellular polymer composite characterized by three distinct directional axes: longitudinal, radial, and tangential. When a conventional fastener penetrates solid timber, extensive hoop stresses accumulate around the core diameter, frequently exceeding the cross-grain tensile cleavage limit of the cellular walls, triggering axial splitting along the vascular bundles.
As an industry-leading China wood self tapping fastener manufacturer and factory, Yu-Huang Electronics Dongguan Co., Ltd. (YH Fastener) has revolutionized thread-forming kinematics through precision-milled Type 17 cut-slot points, optimized 40° to 48° narrow thread profiles, and serrated cutting edges along the initial thread leads. The integrated cut-slot acts as a dynamic chip-carving reservoir, cleanly slicing lignin and cellulose microfibrils rather than simply displacing them. This reduction in radial splitting pressure lowers insertion torque requirements by up to 38% compared to traditional gimlet points, eliminating the need for pilot pre-drilling even in high-density European hardwoods and dense bamboo composites.
Carefully engineered ratio of root diameter to major thread diameter ensures optimal fiber embedment, maximizing the shear cone volume during withdrawal load events while preserving core torsional ductility.
Six-lobe drive profiles guarantee direct radial engagement perpendicular to the rotational vector, eliminating vertical cam-out forces, reducing operator fatigue, and preventing damage to head coatings during automated insertion.
Precision-stamped underside milling pockets self-countersink into solid wood surfaces, cleanly severing protruding fibers and seating the screw head completely flush without edge splintering or tearing.
Unifying automated multi-station cold headers, AI-guided statistical process control, and fully integrated metallurgical heat treatment lines across our 20,000 m² smart manufacturing ecosystem.
At YH Fastener, production efficiency and supply chain resilience are structural imperatives. Operating across three state-of-the-art manufacturing campuses in Dongguan (Headquarters & Precision R&D), Shaoguan (Heavy Forming Hub), and Wuhan (Central Logistics & Bulk Cold-Forging), our infrastructure controls every processing parameter internally. Unlike fragmented workshops that outsource annealing, thread-rolling, and plating to untracked subcontractors, our closed-loop facility operates in strict adherence to IATF 16949, ISO 9001, and ISO 14001 audited quality architectures.
Raw wire coils (high-grade C1022A carbon steel, 10B21 boron alloy steel, or Austenitic 304/316 stainless grades) undergo in-house spheroidize annealing, ultrasonic cleaning, and micro-crystalline zinc phosphating. This guarantees uncompromised plastic cold-formability during multi-station heading. Thread forming is executed on ultra-high-speed flat-die and cylindrical rolling lines capable of maintaining pitch micro-tolerances within ±0.015mm at output rates exceeding 450 units per minute.
Eddy-current flaw detection and spectral metallurgical analysis ensure clean grain alignment and zero internal micro-fissures in raw coil feedstock.
Progressive closed-die cold forging forms drive recesses and specialized underhead geometries while continuously refining metallurgical grain boundaries.
Computer-monitored atmosphere mesh belt carbonitriding provides a glass-hard outer case (550-650 HV0.3) supported by a flexible, ductile core (320-400 HV10).
High-speed 360-degree glass plate optical sorting equipment checks shank straightness, drive depth, thread concentricity, and surface defects at 800 pcs/min.
Field-proven fastener configurations tailored to the rigorous chemical, mechanical, and climatic demands of modern commercial construction.
Long-format structural wood screws (up to 600mm lengths) serving as cross-layer tension and shear reinforcements in Cross-Laminated Timber (CLT) panels and Glulam portal frames, replacing labor-intensive steel gussets.
Specially adapted twin-lead and Hi-Lo self-tapping threads engineered for medium-density fiberboard (MDF), particleboard, and dry softwoods, preventing core blowout while delivering maximum strip-out torque thresholds.
Forged from vacuum-passivated AISI 316 / A4 stainless steel with reverse-thread collars that pull decking boards firmly against joists while preventing mushrooming in exotic tropical hardwoods (Ipe, Cumaru, Teak).
Equipped with high-performance multi-layer ceramic fluoropolymer coatings engineered specifically to resist the aggressive copper-ion degradation present in modern pressure-treated wood preservatives.
Full metallurgical breakdown of industrial wood self-tapping fasteners produced in our Dongguan and regional manufacturing hubs.
| Property / Characteristic | C1022A Structural Carbon Steel | 10B21 Boron Enhanced Alloy | AISI 304 (A2) Stainless | AISI 316 (A4) Marine Stainless |
|---|---|---|---|---|
| Primary Application | General Timber, Interior Joinery, Drywall | Heavy CLT, Timber Bridges, Earth Anchor | Exterior Decking, Pergolas, Humid Cladding | Marine Piers, Salt-Spray Enclosures, Chemical |
| Surface Hardness (Case) | 540 – 650 HV0.3 | 560 – 680 HV0.3 | Work-hardened ~350 HV | Work-hardened ~360 HV |
| Core Hardness | 300 – 390 HV10 | 340 – 420 HV10 | Annealed Ductile Core | Annealed Ductile Core |
| Bending Angle Resilience | ≥ 45° without fracture | ≥ 45° to 60° high ductility | ≥ 90° extreme plastic reserve | ≥ 90° extreme plastic reserve |
| Standard Surface Finishes | Yellow Zinc, Cr3+ Clear, Black Oxide | Ruspert 1000h-1500h, Dacromet, GeoMet | Passivated, Electro-Polished | Electropolished, Fluoropolymer |
| Neutral Salt Spray (ASTM B117) | 48h to 120h (White Rust) | 1,000h to 2,500h (Red Rust Free) | Immune to general atmospheric rust | Immune to harsh coastal & acid environments |
| Compliance Certification | CE EN 14592 RoHS | ETA Approved CE | ISO 3506-1 REACH | DIN EN 10088 Marine Grade |
How YH Fastener bridges domestic Chinese manufacturing velocity with stringent Western regulatory frameworks and just-in-time logistics architectures.
Every commercial production batch is issued with verified EN 10204 3.1 Mill Test Certificates, full PPAP Level 3 packages (Control Plan, FMEA, Gage R&R), and independent laboratory salt-spray verification test reports.
We operate customized Vendor Managed Inventory (VMI) and safety-stock reservation schemes in Dongguan, ensuring guaranteed shipment turnaround within 48 hours for long-term contract partners across the globe.
In-house high-speed cartoning and blister-sealing lines allow complete white-label branding, customized EAN/UPC barcoding, multilingual labeling, and weather-sealed outer master pallets configured for direct-to-shelf delivery.
Anticipating structural decarbonization, advanced robotic installation environments, and next-generation composite timber alloys.
Developing molecular wax coatings synthesized from bio-based plant esters that reduce drive insertion torque by 45% without interfering with timber adhesive bonding in laminated post-and-beam connections.
Precision-collated screw strips engineered with zero-burr head recesses and precise shank concentricity tolerances (±0.01mm) specifically tailored for multi-axis CNC robotic gantry screwdrivers in automated modular house factories.
Deploying advanced nano-ceramic and zinc-flake hybrid matrices that deliver over 2,500 hours of ASTM B117 salt spray endurance with completely non-toxic, Cr-free, and PFAS-free lifecycle profiles.
Authoritative technical guidance compiled by our senior sales engineering team to assist international buyers, QA managers, and structural designers.
Unlike trading intermediaries or localized assembly workshops, YH Fastener (Yu-Huang Electronics Dongguan Co., Ltd.) brings over 30 years of in-house manufacturing experience across 20,000 m² of certified industrial floor space. We control the entire metallurgical flow: spheroidized annealing, high-speed multi-station cold heading, precision thread rolling, computerized continuous atmosphere heat treatment, and automated optical laser sorting. Operating under IATF 16949 and ISO 9001 quality frameworks, we deliver absolute batch-to-batch consistency with failure rates under 1 PPM.
The Type 17 point features an axially cut flute milled directly into the tapered lead thread. When the screw begins rotational engagement, this sharp flute functions like a chip-cutting drill bit, cleanly shaving and extracting localized wood fibers into the slot channel. By relieving internal hydraulic wood-cell hoop pressure, the radial wedging force is reduced by nearly 40%, allowing direct driving into timber edges and brittle hardwoods without splintering.
Standard electro-galvanized coatings quickly break down when exposed to the high concentration of galvanic copper ions in Alkaline Copper Quat (ACQ) lumber. We strongly mandate either our multi-layer Ruspert / ceramic zinc flake finish (passing 1,500+ hours ASTM B117 salt spray) or high-grade austenitic stainless steel (AISI 304 for general exterior construction, AISI 316 for seaside or heavy chemical contact).
In accordance with EN 14592 testing protocols using standard C24 structural softwood (characteristic density $\rho_k = 350\text{ kg/m}^3$), our deep-thread structural wood fasteners deliver a characteristic withdrawal parameter ($f_{ax,k}$) ranging from 12.5 to 14.8 N/mm². When driving into engineered Glulam or hardwood species, our dual-angle thread forms achieve higher pull-out resistance due to maximized mechanical shear engagement within the wood matrix.
Yes. Our in-house tool and die design department engineers custom carbide heading dies within 7 to 10 working days. We support non-standard head diameters, under-head milling ribs, double-thread pitches, partial unthreaded shanks with reaming knurls, and proprietary tamper-resistant security drive recesses based on your 2D engineering drawings or 3D STEP models.
Every commercial container shipment is supported by comprehensive documentation: EN 10204 Type 3.1 Mill Inspection Certificates (detailing raw material chemical heat analysis and core/surface Vickers hardness), full batch dimensional inspection records, torque-to-failure test graphs, plating thickness measurements via X-ray fluorescence, and salt-spray chamber test verifications.
Explore our specialized industrial series including tamper-resistant heads, integrated EPDM washer systems, and black oxide high-tensile machine assemblies.